 PartDorinUpload RFQRFQ
PPAP vs FAI vs ISIR: an automotive supplier approval guide
PPAP, FAI and ISIR can overlap in dimensional and sample evidence, but they do not represent the same approval decision or documentation package.
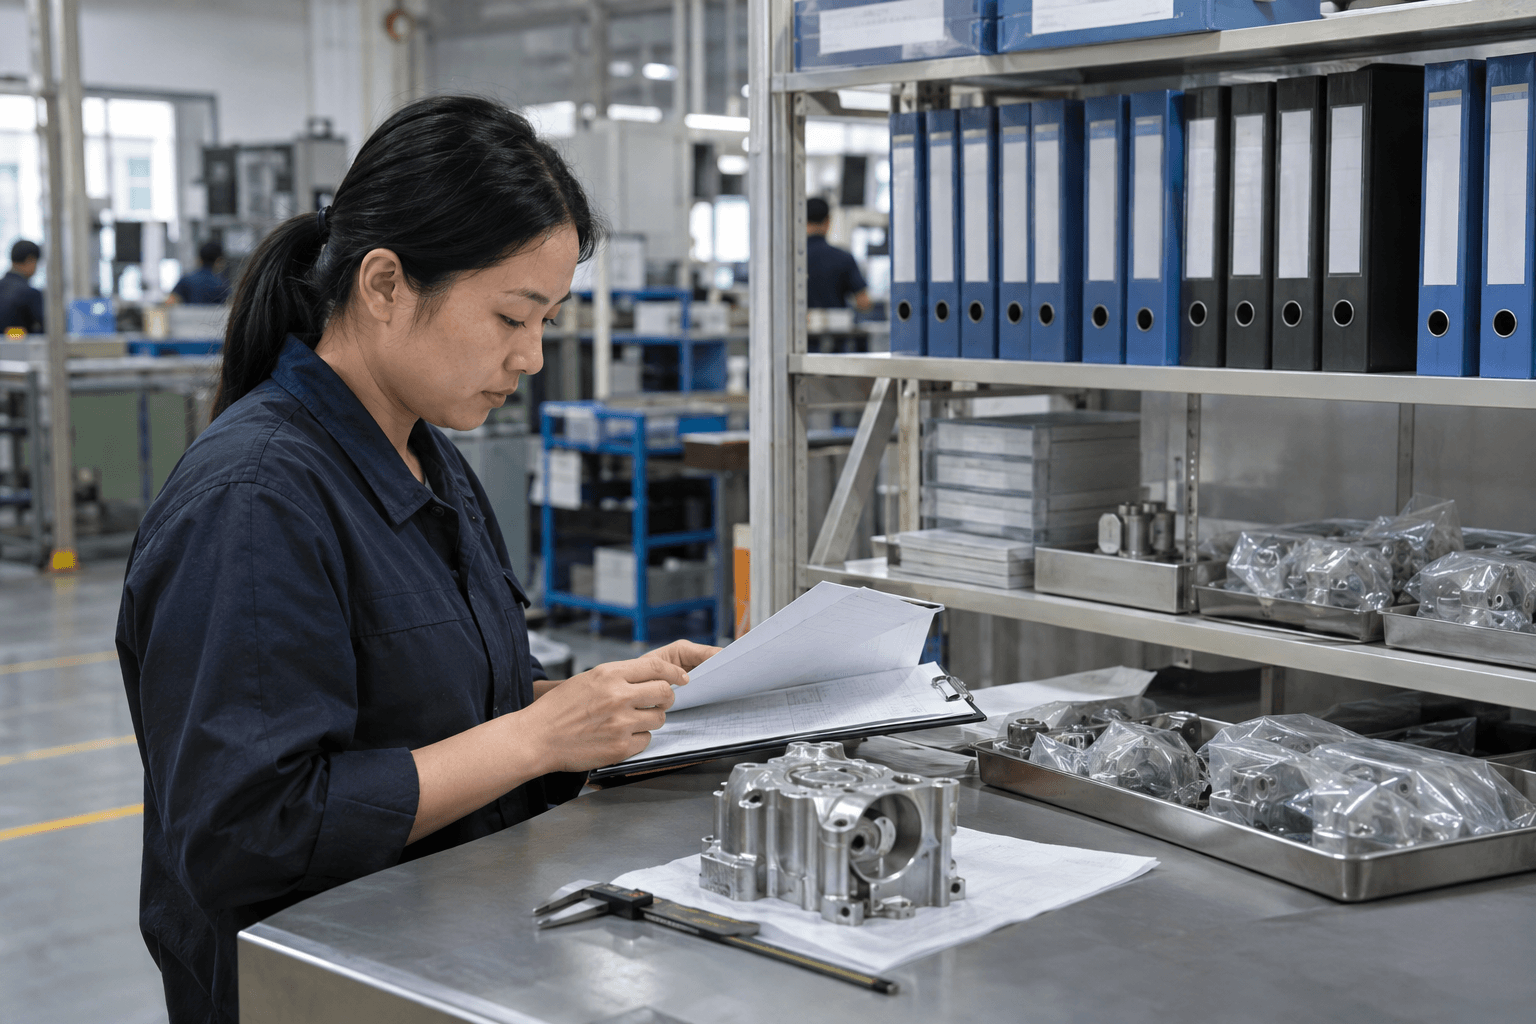
FAI checks the first produced item or initial output against defined requirements. ISIR records initial-sample inspection results in a format commonly used in European automotive supply. PPAP is a broader production-part approval process intended to show that requirements are understood and the production process can repeatedly make conforming parts at the quoted production conditions.
PPAP vs FAI vs ISIR: the short answer
FAI, ISIR, and PPAP can all contain measurements from initial parts, but they answer different approval questions. First article inspection checks an initial produced item against specified characteristics. An initial sample inspection report records results for initial samples, often in a customer or European automotive format. Production Part Approval Process evaluates a broader production-part and process evidence package.
The terms should not be treated as interchangeable certificates. Their exact scope comes from the customer, purchase order, drawing, quality agreement, applicable manual, and customer-specific requirements. The buyer should state which process applies, the required submission level or evidence list, who can approve it, and which events trigger resubmission.
The Automotive Industry Action Group describes PPAP as the industry standard for defining production-part approval so engineering design records and specification requirements can be met consistently during an actual production run at production rates. That is broader than measuring one convenient sample.
What is first article inspection?
First article inspection, or FAI, verifies an initial production output against defined requirements. The “article” should be traceable to the part number, drawing revision, material, process, tooling, and production conditions under review. The report commonly records ballooned drawing characteristics, specified measurements, material or process evidence, and any nonconformance.
FAI is useful when a part is new, a drawing changes, tooling moves, a process changes, production resumes after a long gap, or the customer otherwise requires renewed evidence. The trigger and depth should be defined by the buyer. A supplier may use “FAI” informally for a dimensional report, while a customer may expect a controlled form and full characteristic accountability.
An FAI result demonstrates conformity of the inspected output under stated conditions. It does not by itself prove long-term capability, production rate, process stability, or complete system validation. It also does not release deviations unless the customer’s authorized process explicitly approves them.
What is an ISIR?
ISIR means initial sample inspection report. It is widely used in European automotive supply and is associated with recording initial-sample results against requirements. The document may include part and drawing identification, sample reason, characteristic results, material evidence, process information, and supplier or customer disposition.
Because companies use different forms and submission expectations, the label “ISIR” does not define one universal package. Ask which customer format, VDA requirement, submission level, and additional evidence apply. A spreadsheet titled ISIR is not automatically sufficient for a customer operating a defined product-and-process approval procedure.
The ISIR should identify the samples and production conditions represented. Sample-room parts, prototype tooling, or hand-adjusted output may be valuable during development, but they should not be presented as series-production evidence unless the customer has agreed to that scope.
What is PPAP?
PPAP is a production-part approval process used to show that customer engineering and specification requirements are understood and that the planned manufacturing process can repeatedly produce conforming parts under actual production conditions. It connects product evidence with process evidence rather than relying on final measurements alone.
A PPAP package can include design records, authorized changes, engineering approvals, process flow, process failure mode and effects analysis, control plan, measurement-system evidence, dimensional results, material and performance results, initial process studies, qualified-laboratory records, appearance approval where applicable, sample parts, master sample, checking aids, customer-specific evidence, and a part submission warrant. The required submission level controls what is submitted to the customer, not necessarily what the supplier must complete and retain.
Do not copy a generic package list into every aftermarket RFQ. Many distribution purchases do not operate under an OEM PPAP program. Request PPAP only when the customer, contract, product-development route, or risk requires it. Otherwise define a proportionate sample and production-approval package without claiming it is PPAP.
Purpose, scope, and output comparison
FAI primarily asks whether the initial produced item conforms to the specified characteristics. ISIR records initial-sample inspection evidence within the applicable customer or regional procedure. PPAP asks whether product and process evidence supports production approval under defined conditions.
Their outputs can overlap: the same dimensional results may support an FAI, appear in an ISIR, and form one element of a PPAP package. Overlap does not make the approvals equivalent. PPAP normally reaches further into process planning, control, capability, and customer disposition.
- FAI focus: first produced output, full or defined characteristic verification, traceable result.
- ISIR focus: initial sample result and related submission evidence under the applicable customer format.
- PPAP focus: production-part and process approval, including multiple linked quality-planning records.
- Shared need: correct part, revision, specification, measurement method, sample identity, and customer decision.
- Key distinction: evidence scope and approval authority, not the document title printed on the cover.
Define the submission before requesting a quotation
PPAP work can affect tooling, metrology, laboratory testing, production-run quantity, schedule, and cost. State the expectation during RFQ so suppliers can evaluate feasibility. A late request for a Level 3 package after the product price is agreed can create conflict because the original quotation may not include the required run, testing, or documentation.
Identify the customer, part number, drawing revision, annual volume, special characteristics, applicable manual revision, submission level, customer-specific requirements, language, portal, sample quantity, timing, and approval authority. Name any required laboratories, test standards, capability studies, or material-data systems.
The IATF customer-specific requirements library shows why a general IATF statement is not enough: automotive customers publish additional requirements that can change the expected product-approval process. Verify the current customer document for the actual program.
Submission levels do not describe product quality grades
PPAP submission levels describe which evidence is submitted or made available under the applicable PPAP rules and customer instruction. They are not “quality levels” of the part. A Level 3 submission does not automatically mean the product is better than a part handled under Level 1; it means the customer requested a different evidence submission.
The supplier still needs to perform required activities and retain applicable records. The customer can request additional elements, waive items, or specify a different level. Never assume a standard default overrides a purchase order or customer-specific requirement.
Ask for the formal customer disposition: approved, interim or otherwise defined, rejected, or pending. A package emailed to the buyer is “submitted,” not necessarily “approved.” Keep the signed or portal-recorded disposition connected to the part and revision.
Share the reference, vehicle application and target quantity so the technical and packing questions can be reviewed against your actual order.
Upload Your RFQProduction samples must represent the intended process
Approval evidence becomes weak when samples come from a different route than planned production. Record the manufacturing site, line, tooling, cavity, material batch, operators or shift where relevant, process settings, and run quantity. Explain any prototype or temporary condition rather than hiding it.
PPAP is meant to evaluate output from the intended production process. The quoted production rate and actual run conditions can matter. An FAI also needs a declared sample source; otherwise the buyer cannot know whether the result represents the process that will make future orders.
Keep sample parts identified and protected. If a master sample is required, control its approval, storage, validity, and replacement. Physical samples without stable document links become unreliable when drawings or tooling change.
Measurement and test evidence needs method control
A dimensional report is credible when it names the characteristic, nominal value, tolerance, result, instrument or method, unit, and sample. Measurement equipment should be suitable for the tolerance, calibrated, and used through an agreed datum strategy. Ambiguous drawing interpretation should be resolved before the report is completed.
Material and performance records should identify the exact part or batch, test method, acceptance criteria, laboratory, date, and result. A generic supplier certificate or unrelated catalog test does not establish conformity for the submitted part. Where an accredited laboratory or customer-approved facility is required, confirm the scope.
Measurement-system analysis and process studies have different purposes from final inspection. Do not substitute one for another. A few conforming pieces do not prove process capability, and a capability statistic does not excuse an out-of-specification sample.
Handle deviations and interim status openly
If a characteristic does not meet the requirement, record the nonconformance and use the customer’s deviation or concession process. Do not alter the drawing value, omit the characteristic, or mark it acceptable based on an informal discussion. The disposition should identify the exact part, revision, quantity, period, and conditions covered.
Interim approval can allow limited activity while defined actions remain open, depending on the customer system. It is not permanent approval. Track expiration, quantity limits, corrective actions, and resubmission date. Do not ship beyond the authorized scope.
A rejected submission should trigger containment and a structured response. Determine whether the problem is product, process, measurement, documentation, or misunderstanding. Correct the cause and resubmit under the customer’s rules rather than simply replacing a page.
Change control and resubmission triggers
Approval applies to a controlled product and process state. Drawing changes, material changes, new tooling, repaired or transferred tooling, production-site moves, new suppliers, process changes, long inactivity, or other events can trigger notification and resubmission. The exact triggers come from the applicable manual and customer requirements.
Build a change-notification rule into the purchase agreement. The supplier should not implement a change that can affect the approved product without the required buyer review. This is especially important when a distributor uses the same supplier part number across repeat orders and assumes the internal construction remains unchanged.
Keep revision history and effective dates. Receiving and shipment inspection should be able to distinguish old and new approved versions. Mixed versions require explicit control rather than silent consumption.
How aftermarket distributors should use these methods
Most aftermarket distributor orders do not need a complete OEM-style PPAP for every catalog line. The practical goal is proportional evidence. A standard service part may use an approved sample, controlled specification, category-specific test record, packing approval, and pre-shipment inspection. A custom safety-relevant component or customer-nominated program may require much deeper approval.
Ask what decision the evidence must support. If the question is “does this first sample match our drawing?”, an FAI-style report may be appropriate. If the customer requires a European initial-sample submission, use its ISIR or PPA requirements. If the program requires production-process approval under AIAG and customer rules, plan the PPAP from RFQ onward.
PartDorin does not present a generic factory document as universal product approval. Use the supplier-qualification page to request evidence tied to the exact part, plant, process, and destination.
Buyer checklist for PPAP, FAI, or ISIR requests
- Name the customer and approval procedure.
- State part number, drawing, revision, specification, and authorized changes.
- Define FAI, ISIR, PPAP, or a custom evidence package without mixing labels.
- State submission level, elements, sample count, language, portal, and due date.
- Identify special characteristics, methods, laboratories, and capability expectations.
- Confirm intended production site, tooling, line, cavity, material, and run conditions.
- Define deviations, interim approval, rejection, and resubmission handling.
- List change-notification and repeat-submission triggers.
- Identify who can approve and what record proves the disposition.
- Carry the approved baseline into production, labels, packing, and shipment inspection.
Include this checklist with the custom automotive parts RFQ so suppliers can evaluate technical and documentation scope before committing to price and timing.
Frequently asked questions
Is FAI part of PPAP?
Initial-part measurements can support PPAP dimensional evidence, but “FAI” and “PPAP” are not identical. The required relationship depends on the customer procedure. PPAP contains broader product-and-process evidence and a customer approval disposition.
Is ISIR the same as a dimensional report?
Not necessarily. An ISIR commonly includes dimensional results, but the required submission can also include material, process, sample, and customer-specific evidence. Ask for the applicable format and approval procedure rather than assuming any dimensional spreadsheet is an ISIR.
Does an IATF 16949 certificate replace PPAP?
No. IATF 16949 certification concerns the organization’s automotive quality-management system and certified scope. PPAP is a part- and process-specific approval activity under customer requirements. Neither automatically proves the other.
When should PPAP be requested from an aftermarket supplier?
Request it when the customer, contract, development program, product risk, or quality agreement requires PPAP and the supplier can plan the work from RFQ onward. For ordinary catalog purchases, a proportionate documented approval plan may be more appropriate.
Conclusion: request the approval decision you actually need
PPAP vs FAI vs ISIR is not a contest between document names. Start with the customer decision, then define the required product, process, sample, measurement, and approval evidence. Keep every result tied to the correct revision and intended production route.
Send PartDorin the drawing, application, volume, customer requirement, submission expectation, and target timing through the RFQ page. The review can identify open evidence and commercial scope without claiming approval before the responsible customer has issued it.
Discuss the requirements for your next order.
Send your part references, vehicle applications, target quantities, destination market and any inspection or packing priorities. PartDorin will review the information needed for a focused quotation.
Send Your Requirements